

Views: 0 Author: Site Editor Publish Time: 2026-08-10 Origin: Site


Residual internal stress and surface distortion compound costs rapidly in sheet metal and steel plate processing. Defects like edge waves, center buckles, coil set, and crossbow act as silent saboteurs on the fabrication floor. They cause catastrophic tolerance failures in downstream operations. CNC machining centers struggle to hold dimensions. Laser cutting heads crash into warped plates. Stamping dies suffer premature wear. Robotic welding cells halt due to excessive manual fixturing requirements.
Traditional mechanical straighteners fail to solve these issues. They hit their limits when processing high-yield-strength materials and cannot achieve the tight flatness tolerances required by modern manufacturing. Relying on outdated equipment creates a severe operational bottleneck, driving up manual rework and scrap rates while compromising the structural integrity of final welded assemblies.
The definitive solution is a hydraulic leveling machine. This equipment delivers dead-flat, stress-relieved material consistently. We designed this guide as a technical evaluation matrix to help fabrication engineers specify the correct roll count, hydraulic configuration, and capacity for their specific production environment.
Actuation Precision: Hydraulic leveling machines utilize hydraulic cylinders for entry penetration and dynamic gap control, offering superior responsiveness and overload protection compared to mechanical screw-jack systems.
Roll Count Dictates Capability: Selecting between a 30 roll, 40 roll, or 50 roll hydraulic leveling machine is strictly dictated by material thickness, yield strength, and the required flatness tolerance.
Structural Deflection is the Enemy: Effective leveling requires robust intermediate support rolls to prevent work roll deflection under high tonnage, ensuring uniform pressure across the entire plate width.
Downstream ROI: The primary financial justification for a hydraulic sheet leveler for steel plates is the elimination of thermal distortion during laser cutting, the establishment of a true datum surface for CNC machining, and the reduction of fixturing time in automated welding cells.

Mechanical straighteners rely on static screw jacks to set roll gaps. They lack dynamic response. When thicker or harder material enters the pinch rolls, mechanical systems often jam. The immense upward force transfers directly into the machine frame, frequently causing catastrophic structural damage or snapping the drive shafts. Hydraulic cylinders change this dynamic entirely. They adjust entry penetration instantly and manage exit gaps with extreme precision. This allows for aggressive initial yielding of the metal sheet without risking the equipment.
Advanced servo-hydraulic systems take this control further. They provide real-time tilt and gap adjustments while under massive operational loads. Linear Variable Differential Transformer (LVDT) sensors detect material variations and command the proportional valves to compensate in milliseconds. Some facilities opt for hybrid configurations. These systems use hydraulic cylinders for entry penetration combined with a motor and screw-jack system for exit penetration. Hybrids serve as a viable middle-ground for shops that need hydraulic overload protection but have strict budget constraints.
Hydraulic overload protection mechanisms are non-negotiable on the shop floor. They prevent catastrophic machine damage. If an anomalous material thickness—like a double-fed sheet or a heavy weld seam—enters the machine, the hydraulic pressure spikes. Relief valves open instantly. The cylinders retract, dropping the lower roll bank. This immediate release saves the work rolls, bearings, and drive train from destruction.
Metal retains a physical memory of its manufacturing process. Rolling, coiling, and rapid cooling introduce uneven stresses across the grain structure. To flatten the metal permanently, you must manipulate the Bauschinger effect. This metallurgical principle states that subjecting a metal to alternating bending cycles alters its yield characteristics. The leveling machine bends the material back and forth over a series of offset rolls. Each bend pushes the material past its plastic yield point. The radius of the bends decreases progressively from the entry to the exit. This sequence neutralizes trapped internal stresses.
Visually flat material from a standard straightener deceives operators. It may look flat sitting on a pallet, but it still contains trapped internal stress. When you subject this material to heat during laser cutting or welding, the stress releases. The metal warps instantly, often ruining the part. Material removal during CNC milling causes the exact same reaction. True leveling prevents this phenomenon entirely. It creates a stable, stress-free datum surface that remains dead-flat regardless of aggressive downstream processing.
Work rolls cannot withstand leveling forces alone. Pushing high-tensile steel past its yield point requires immense downward pressure. If you apply this pressure to unsupported work rolls, they will deflect. They bow in the center. This bowing creates uneven pressure across the plate width, resulting in severe edge waves or center buckles that ruin the material.
Engineers solve this deflection problem with an extra row of intermediate backup rolls. You position these heavy-duty backup flights directly between the upper and lower rows of leveling work rolls and the main support frame. This multi-tier arrangement creates a rigid, unyielding structure. It prevents the primary work rolls from deflecting under extreme tonnage. Uniform pressure remains constant across the entire width of the material. This architecture is the backbone of any heavy-duty leveling operation, ensuring that the center of the plate receives the exact same yielding force as the edges.
Heavy fabrication demands robust, unyielding equipment. A 30 roll hydraulic leveling machine fits this profile perfectly. We generally specify this configuration for thicker materials and heavy steel plates. It excels in applications where extreme micro-precision takes a back seat to heavy-duty stress relief. Shipyards, heavy equipment manufacturers, and structural steel fabricators rely heavily on this setup to process thick plates before plasma cutting or submerged arc welding.
The physics of leveling dictate a specific trade-off here. Fewer rolls require larger roll diameters to span the machine frame. Larger diameters increase the maximum thickness capacity. They resist snapping under the immense pressure required to yield thick plates like 25mm mild steel or 15mm AR400. However, this limits effectiveness on thin gauge sheets. Large rolls simply cannot create the tight bending radii necessary to push thin, elastic materials past their yield point.
Mixed-production facilities need versatility above all else. A 40 roll hydraulic leveling machine serves as the ideal middle ground. It handles a moderate range of sheet thicknesses effectively. This configuration provides an excellent balance between deep internal stress relief and fine surface flatness, making it the most common choice for contract manufacturers.
You will find these machines in diverse manufacturing environments. Automotive component suppliers use them to flatten stamped blanks before robotic welding. Standard HVAC fabricators rely on them for large ductwork panels. Manufacturers of medium-gauge structural panels specify this roll count to maintain tight tolerances without sacrificing throughput. It represents the ultimate workhorse configuration for general sheet metal fabrication, easily handling materials from 3mm up to 12mm depending on the frame size.

Certain industries tolerate zero deviation from absolute flatness. Ultra-precision applications require a 50 roll hydraulic leveling machine. This configuration dominates in the processing of thin foils, aerospace components, and electronics manufacturing. The engineering principles here focus entirely on achieving the tightest possible bending radii.
A higher number of smaller-diameter rolls creates more bending cycles within the machine footprint. These smaller rolls bend the material sharply. This is absolutely essential for yielding very thin or highly elastic materials like titanium foils or thin-gauge stainless steel. However, operators must respect the physical limitations of the equipment. This machine is entirely unsuitable for thick steel plates. Feeding heavy plate into a 50-roll system carries a high risk of snapping the small-diameter work rolls instantly, leading to massive repair bills.
Roll Configuration | Primary Application | Typical Material Thickness | Roll Diameter Characteristic | Bending Radius |
|---|---|---|---|---|
30 Roll System | Heavy steel plates, structural components, shipyards | 10mm - 80mm | Large diameter, high rigidity, resists snapping | Wide, suited for thick plate yielding |
40 Roll System | Automotive blanks, HVAC, medium-gauge panels | 3mm - 20mm | Medium diameter, balanced strength | Moderate, highly versatile |
50 Roll System | Aerospace foils, electronics, ultra-precision parts | 0.1mm - 5mm | Small diameter, high cycle count | Extremely tight, suited for thin elasticity |
Sizing a hydraulic sheet leveler for steel plates requires precise mathematical calculations. You cannot guess the required tonnage based on visual inspection. You must calculate it based on three critical factors: maximum material width, maximum thickness, and maximum yield strength. Operational ranges vary wildly across the industry, spanning from 0.1 mm precision foils up to 80 mm heavy armor plates. The yield strength, measured in MPa or PSI, dictates the hydraulic cylinder size, the motor torque, and the overall frame rigidity.
A common pitfall ruins many procurement projects. Facilities size a machine based on the 250 MPa mild steel they process most often. Six months later, they attempt to run 1300 MPa martensitic steel, AR400 wear plate, or high-strength low-alloy (HSLA) steel. The machine stalls. The frame deflects. The rolls bow. Always calculate your tonnage requirements based on the absolute hardest, widest, and thickest material you plan to process.
Identify the maximum width of the plates you will process.
Determine the maximum thickness at that specific maximum width.
Document the highest yield strength (in MPa) of any material entering the facility.
Add a 20% safety margin to the final tonnage calculation to account for unexpected material variations from the steel mill.
Modern leveling requires advanced control interfaces. CNC and PLC systems replace manual handwheels, dial indicators, and operator guesswork. Operators need intuitive HMI screens that allow them to save material profiles. When a specific batch of 5mm aluminum arrives, the operator simply selects the saved recipe. The machine automatically sets the entry penetration, exit gap, and roll tilt. This ensures repeatable setup across different shifts and eliminates operator-induced errors.
Automation integration separates standard machines from high-performance production cells. Look for systems that integrate automated flatness measurement. Laser triangulation sensors or optical topography scanners read the material surface as it exits the machine. They feed this data back to the PLC via high-speed EtherCAT communication. The system provides closed-loop feedback to the hydraulic proportional valves, making micro-adjustments in real-time to guarantee perfect flatness without stopping production.
Pulling heavy plate through offset rolls requires massive rotational force. Drive systems dictate how this force applies to the material. Multi-roll gearbox distribution uses a single large motor to drive all rolls simultaneously via a central distribution box and cardan shafts. While cost-effective, it can cause issues with varying roll speeds due to material elongation as the sheet stretches slightly during the leveling process.
Individual roll drives offer superior performance for sensitive materials. Each roll features its own hydraulic or electric servo motor. This allows for precise torque distribution and independent speed control. Proper torque management prevents material slippage inside the machine. It also eliminates surface marring, scuffing, and chatter marks. If you process polished stainless steel, pre-painted aluminum, or coated metals, individual roll drives are mandatory to protect the surface finish.
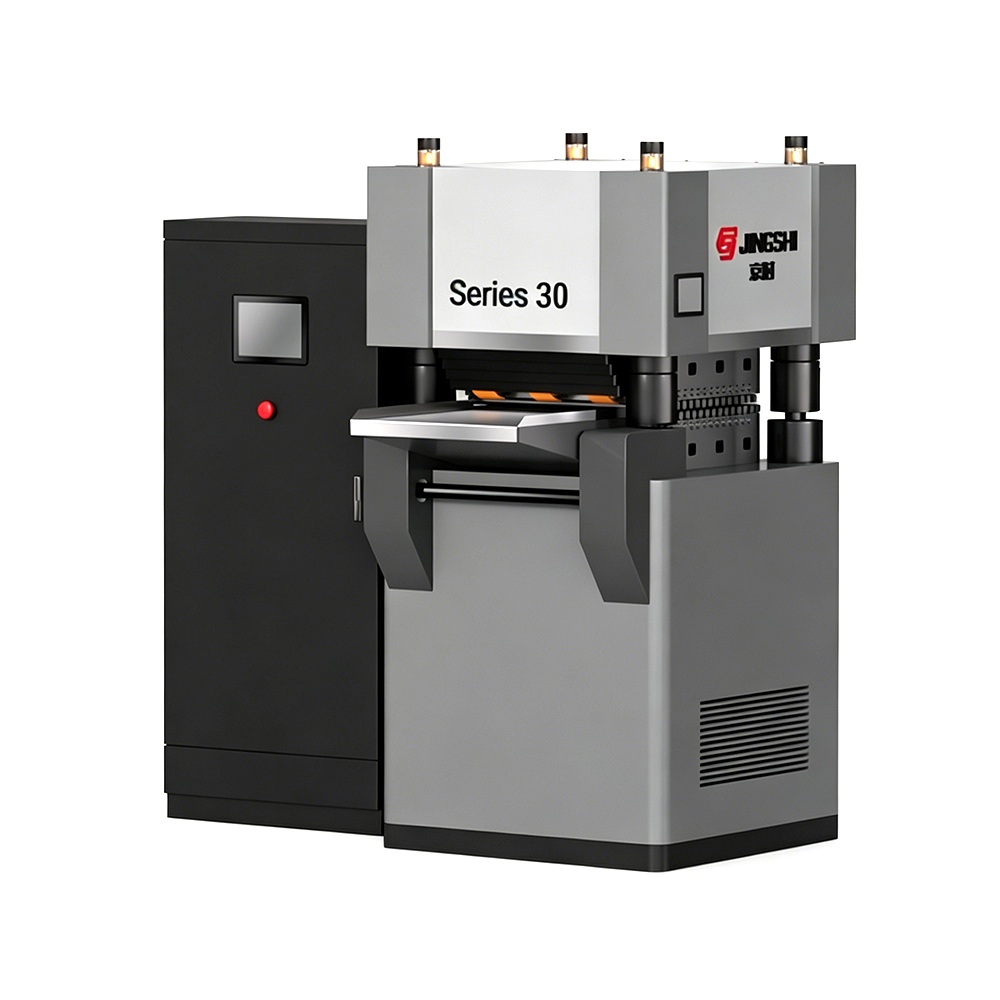
A heavy-duty leveler generates immense dynamic forces. You must isolate the machine from facility vibrations, and you must isolate the facility from the machine. Precision machine leveling is the first step. You cannot place a leveler on an uneven floor and expect flat parts. Utilize precision leveling mounts, heavy-duty leveling wedges, and wedge mounts. These devices ensure the equipment frame sits perfectly aligned to gravity, preventing twisting in the machine base.
The foundation requirements demand serious civil engineering. You cannot bolt a heavy-plate leveler to a standard 6-inch warehouse slab. The concrete depth must accommodate the static weight of the machine and the dynamic shock loads of heavy plates entering the pinch rolls. Deep foundations with heavy rebar reinforcement are standard. Many installations require isolated concrete pads separated from the main floor by vibration-dampening expansion joints and secured with high-strength epoxy grout.
Leveling machines operate in harsh, dirty environments. Maintenance accessibility dictates your overall uptime. Evaluate the ease of maintenance before purchasing. Look for machines featuring quick-change roll cassettes. Slide-out roll assemblies allow maintenance teams to extract the entire work roll bank onto a track system. This makes cleaning, bearing inspection, and calibration safe and efficient, reducing a full-day job to a few hours.
Roll wear is an unavoidable reality. Processing hot-rolled steel introduces abrasive mill scale and debris into the machine. This scale embeds into the work rolls over time, degrading the surface finish. You must establish strict regrinding schedules. Operating with worn or grooved rolls transfers those defects directly onto your finished parts. Daily cleaning protocols using scotch-brite pads and automated lubrication systems prevent debris buildup and significantly extend the lifespan of your roll surfaces.
Purchasing a servo-hydraulic system requires a significant upfront capital expenditure. You must build a calculation model to justify this investment through operational ROI. Track your current hidden costs meticulously. Calculate the exact tonnage of scrapped parts caused by warping during laser cutting. Measure the labor hours wasted on manual hammering, flame-straightening, and excessive weld fixturing.
A precision leveler eliminates these bottlenecks entirely. CNC milling throughput increases because operators no longer waste time shimming warped plates on the machine table. Laser cutters run lights-out without fear of head crashes caused by material spring-back. Robotic welding cells operate efficiently because parts fit perfectly into the jigs every single time. The reduction in scrap and the massive increase in downstream throughput typically offset the initial capital expenditure within the first eighteen months of operation.
Treat the vendor evaluation as critically as the machine specifications. Hardware fails eventually. When a hydraulic valve sticks or a sensor faults, downtime costs compound rapidly. List your critical vendor criteria. Availability of domestic spare parts is paramount. Waiting weeks for overseas shipping destroys production schedules. Remote diagnostic capabilities allow vendor engineers to log into your PLC and troubleshoot faults instantly.
Demand guaranteed response times for hydraulic system failures within your Service Level Agreements (SLAs). Emphasize safety compliance. Verify that the equipment meets CE, OSHA, or specific local safety directives for heavy hydraulic machinery, including light curtains and emergency stop circuits. Finally, never buy off a brochure. Require a physical run-off test. Ship your actual problem materials to the vendor. Make them level your worst-case sheets to your required tolerances before you sign the purchase order.
A hydraulic leveling machine is a highly specific engineered solution. The roll diameter, roll count, and hydraulic tonnage must align perfectly with the metallurgical properties of the material you process. Failing to match the machine to the material results in poor flatness, rejected parts, and damaged equipment.
Your shortlisting logic should follow a strict decision matrix. Choose a 30-roll system for heavy plate and heavy-duty stress relief. Select a 50-roll system for thin foils and ultra-precision gauges. Always prioritize advanced hydraulic controls and closed-loop feedback when processing high-yield materials.
Take the following actions to begin your procurement process:
Audit your current production floor to quantify exact scrap rates and labor hours lost to warped materials.
Document the maximum material yield strengths, widths, and thicknesses your facility processes annually.
Prepare a batch of your most difficult, high-stress sample materials for vendor run-off testing.
Evaluate your facility's foundation depth and vibration isolation capabilities to prepare for installation.
A: Hydraulic leveling machines use hydraulic cylinders to provide dynamic gap control under load. They offer superior internal stress relief and react instantly to material variations. Mechanical straighteners use static screw jacks. They cannot adjust under load and are highly prone to jamming or frame damage during an overload event.
A: Roll selection is inversely proportional to material thickness. Choose a 30-roll machine with fewer, larger rolls for thick, heavy steel plates. Select a 50-roll machine with more, smaller rolls for thin, high-precision sheets. A 40-roll machine serves as a versatile middle ground for medium-gauge materials.
A: Yes, provided the machine is engineered correctly. It requires sufficient hydraulic tonnage to yield the material, robust intermediate backup rolls to prevent work roll deflection, and appropriately sized drive motors to pull the high-friction plate through the bending cycles.
A: These defects stem from residual internal stress. Uneven cooling during the steel milling process or tension from the uncoiling process creates length differentials across the width or length of the sheet. This trapped stress manifests as visible distortion like crossbow, edge waves, or coil set.
A: Relieving internal stress prevents the metal from springing out of shape. During laser cutting, it stops the material from bowing up and crashing into the laser head once the cutting path compromises structural integrity. For CNC milling, it provides a perfectly flat datum surface, ensuring accurate machining tolerances.
A: Maintenance requires daily cleaning to prevent abrasive mill scale and debris from embedding into the rolls. You must perform periodic calibration of the hydraulic tilt and gap sensors. Long-term maintenance involves regrinding the work rolls at intervals dictated by the abrasiveness of your specific materials.

